A Complete Guide to Installation and Commissioning of Carbon Emission Monitoring Systems
Yicai Technology Industry Observation: Against the backdrop of the continued advancement of the "dual carbon" goals, carbon emission monitoring is gradually shifting from "having data to report" in corporate compliance reporting to "having data to manage" in production operations. For key emission units, industrial parks, energy enterprises, and core supply-chain enterprises, online greenhouse gas monitoring is not only the data foundation for carbon accounting but also an important tool for identifying energy-intensive processes, optimizing combustion efficiency, calculating product carbon footprints, and conducting Scope 3 emission management.
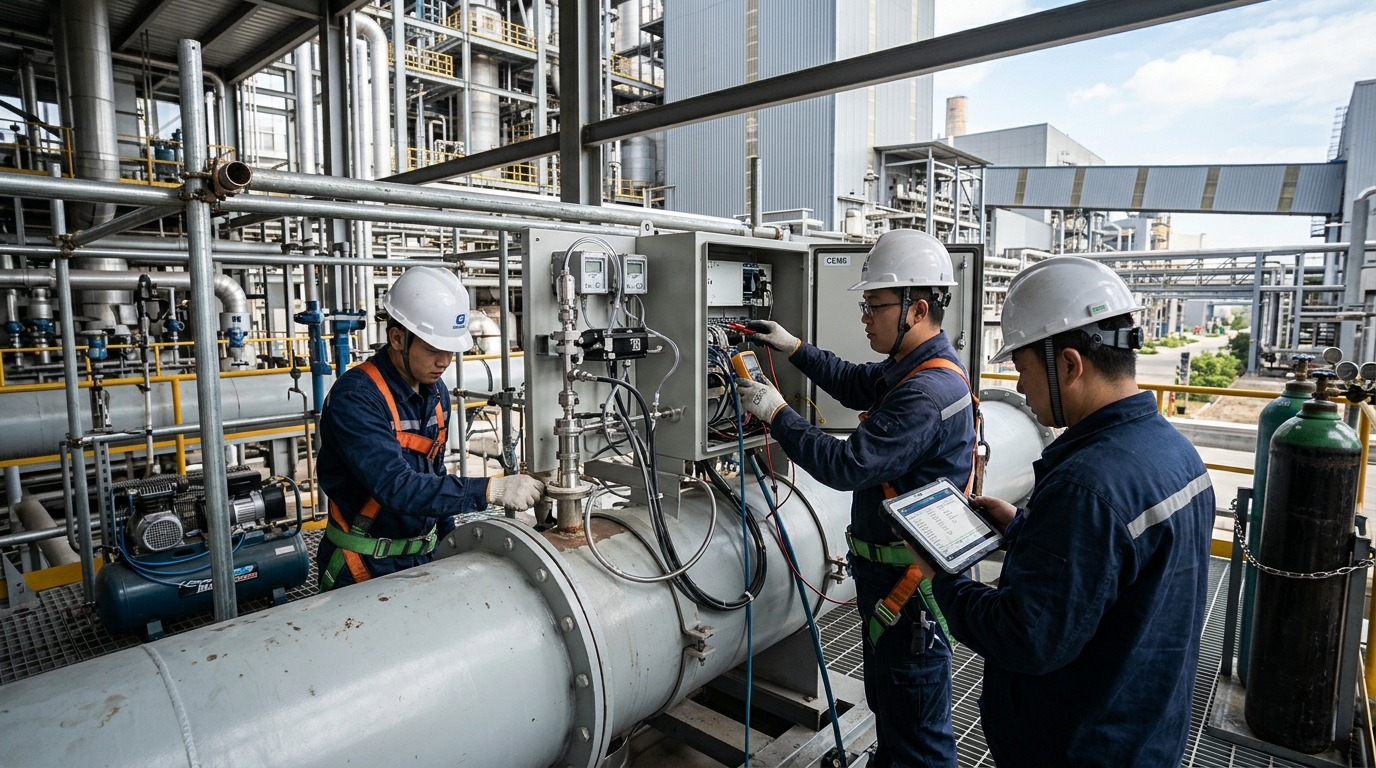
However, in actual implementation, equipment selection, installation locations, commissioning and calibration, routine maintenance, and data fault handling often determine the credibility of final monitoring results. This article outlines the implementation path of carbon emission monitoring systems from a practical perspective. Focusing on key aspects such as carbon accounting, carbon footprints, greenhouse gases, and online monitoring, it describes installation steps, commissioning methods, routine maintenance, and key points for common fault troubleshooting. The parameters and cases in this article are based on industrial flue gas, plant boundary, and stationary emission source monitoring scenarios, for reference by corporate environmental protection, energy, metrology, production, and digital management personnel.
I. Monitoring Boundaries and Pre-Installation Preparation
Before conducting carbon emission monitoring, the monitoring boundary must first be clearly defined. Corporate greenhouse gas emissions are typically categorized into Scope 1, Scope 2, and Scope 3. Scope 1 includes fuel combustion, process fugitive emissions, and direct emissions from mobile sources; Scope 2 mainly refers to indirect emissions from purchased electricity, heat, etc.; Scope 3 covers value-chain emissions such as raw material procurement, logistics and transportation, product use, and end-of-life disposal. Online monitoring equipment primarily serves flue gas emissions from stationary sources under Scope 1, and can also assist in identifying process fugitive emissions, plant boundary leaks, and abnormal operating conditions.
In terms of carbon accounting methods, common corporate approaches include the emission factor method, material balance method, and direct measurement method. The emission factor method is suitable for enterprises with complete energy consumption and raw material input data but a weak foundation for continuous flue gas monitoring; the material balance method is suitable for industries with pronounced process emission characteristics, such as cement, steel, and chemicals; the direct measurement method relies on online greenhouse gas monitoring systems and is especially applicable to scenarios with large emission fluctuations, complex operating conditions, or the need to support product carbon footprint accounting. Regardless of the method adopted, data quality requirements should be implemented across three levels: traceability, verifiability, and auditability.
Key Tip: Fixed-source flue gas sampling points should avoid eddy currents, bypasses, diameter transitions, and branch pipe confluence areas. It is generally recommended that the upstream straight duct length at the sampling point be no less than 10 times the stack diameter, and the downstream straight duct length be no less than 4 times the stack diameter.
The first task in pre-installation preparation is site selection. If constrained by site conditions, at least the minimum straight duct length requirements specified by relevant standards should be met, and representativeness should be confirmed during commissioning through velocity profile testing. For enterprises with multiple branches sharing a stack, monitoring points should preferably be installed at the main discharge outlet, with auxiliary points set up at key branches to distinguish the contributions of different processes.
Before installation, platform, power supply, communication, and safety conditions must also be confirmed. The sampling platform should meet personnel inspection and equipment maintenance requirements; platform guardrail height should typically be no less than 1.2 meters, with anti-slip treads and maintenance space provided. It is recommended that equipment cabinets be powered by 220 V AC. Important systems should be equipped with uninterruptible power supplies with a backup duration of no less than 10 to 30 minutes to avoid data interruption caused by short-term power outages. Grounding resistance is generally controlled within 4 ohms. The communication network can use industrial Ethernet, fiber optics, 4G, or 5G depending on site conditions. In hazardous areas, sampling probes, junction boxes, and cabinets must meet the corresponding explosion-proof rating requirements.
II. Installation Steps: From Sampling Probe to Data Gateway
Carbon emission online monitoring systems typically consist of sampling probes, heated sample lines, pre-treatment units, gas analyzers, flow and process sensors, data acquisition gateways, standard gases, and cabinets. If greenhouse gases such as carbon dioxide, methane, and nitrous oxide are monitored simultaneously, the measurement principle—non-dispersive infrared, Fourier-transform infrared, tunable diode laser absorption, or mass spectrometry—should be selected according to the measurement range. During installation, the flange opening location should first be confirmed, avoiding weak insulation areas or positions directly facing flue gas dead zones. After opening, standard flanges should be added, and sealing and insulation restoration should be properly completed.
Sampling Probe Installation
Sampling probe installation is the foundation for stable system operation. The probe insertion depth should match the stack diameter, velocity profile, and sampling cross-section, typically inserted near the center of the stack or arranged according to the designed cross-section. The probe should face the flue gas flow direction and avoid being directly exposed to high-velocity erosion areas to reduce dust abrasion and blockage risks. For flue gas with high dust content, probes with reverse-purge functions should be preferred. The purge interval can be set to 10 to 30 minutes; the purge gas source can be compressed air or nitrogen, with pressure stabilized in the range of 0.2 to 0.6 MPa.
Heated Line Routing
Heated line routing requires strict control of slope and insulation. The length of heated sample lines should be minimized; it is generally recommended not to exceed 30 to 50 meters. Excessive length will increase response time, temperature attenuation, and condensation risk. The installation slope of the line should preferably be maintained between 1% and 3%, avoiding U-shaped bends or low points where liquid can accumulate. The segment from the probe to the cabinet should be fully heated, with temperature typically controlled at 120 to 160 degrees Celsius to prevent moisture in the flue gas from condensing and adsorbing gases such as carbon dioxide and methane. The spacing between line supports can be set at 1.5 to 3 meters. Protective sleeves should be added when the line passes through insulation layers or platform edges.
Pre-treatment Unit Installation
Pre-treatment unit installation should be determined based on the analyzer principle. If dry-basis measurement is used, cooling, water removal, and drying modules should be configured so that the dew point of the gas entering the analyzer meets equipment requirements; a common control target is a dew point no higher than -10 degrees Celsius. If wet-basis measurement is used, flue gas moisture must be retained and humidity measured simultaneously, then dry-basis concentration is calculated through algorithms. Regardless of the method, filter precision should match the dust concentration. Common first-stage filter precision is 5 to 10 micrometers, and second-stage filtration can further reduce it to 0.5 to 1 micrometer. The sampling pump flow rate is typically controlled at 0.5 to 2 liters per minute; the specific value should be set according to the analyzer inlet flow requirement.
After installation of analyzers, process sensors, and data gateways, labeling and cable management should be performed. Gas analyzer cabinets should avoid direct sunlight and rain ingress; indoor temperature should preferably be controlled at 5 to 40 degrees Celsius, with relative humidity below 85%. Installation locations for carbon dioxide, methane, and other analyzers should be away from equipment with strong vibration and high-temperature heat sources. Data acquisition gateways should support data aggregation at 1 second, 1 minute, or 15 minutes and have breakpoint retransmission capability. When connecting to enterprise management platforms or regulatory platforms, protocols such as Modbus TCP, OPC UA, MQTT, or HJ 212 can be used; specific interfaces must be confirmed during project design.
III. Commissioning Methods: Static First, Then Dynamic; Single Point First, Then System
The commissioning phase should follow the principle of "static first, then dynamic; single point first, then system." Static commissioning includes power-on inspection, wiring verification, valve status confirmation, and standard gas connection. Dynamic commissioning includes tightness testing, zero calibration, span calibration, response time testing, process matching testing, and network connection testing. Commissioning records should include time, personnel, equipment number, standard gas concentration, environmental conditions, raw data, and final parameters to facilitate traceability of subsequent carbon accounting data.
Tightness Testing
Tightness testing is the first step to avoid data distortion. The system can apply slight negative pressure at the sampling pump inlet or positive pressure at the outlet side and observe pressure changes. Generally, the pressure change of the system within 10 minutes should not exceed the allowable range, and the leakage rate should preferably be controlled within 0.05% volume per minute. If rapid pressure drop is found, the probe, heated line, filters, valve assembly, pump diaphragm, and cabinet interfaces should be checked section by section. Common leakage points include flange gaskets, quick-connect fittings, drain valves, and heated tube joints.
Zero and Span Calibration
Zero and span calibration directly affect the calculation of carbon dioxide concentration and greenhouse gas emissions. Zero gas is usually high-purity nitrogen or synthetic air; span gas can be standard carbon dioxide, with concentration selected according to actual operating conditions, such as 5%, 10%, 20%, or higher. For low-concentration components such as methane and nitrous oxide, ppm-level standard gases should be used, for example, 5 to 100 ppm methane standard gas. During commissioning, zero drift and span drift should be recorded. Typically, 7-day zero drift and span drift are required not to exceed ±2% of full scale, linearity error not to exceed ±2% full scale, and repeatability not to exceed 1% full scale.
Response Time and Network Testing
Response time testing is used to evaluate the system's ability to track changes in operating conditions. Taking the time required for the analyzer reading to reach 90% of the target value when standard gas is introduced as an example, the T90 of a fixed-source flue gas online monitoring system is typically required to be no more than 60 seconds, and T10 no more than 20 to 30 seconds. If the response time is too long, it may affect data accuracy during boiler start-up/shutdown, load fluctuations, and abnormal emissions. Common causes of slow response include excessively long lines, insufficient pump flow, filter blockage, low heated-line temperature, and condensation in pre-treatment.
Network connection and data quality testing are important final steps of commissioning. The system should be able to upload minute values, hourly values, and 15-minute averages according to the set cycle and generate valid data completeness indicators. For carbon accounting and regulatory reporting scenarios, the valid data capture rate is generally recommended to be no less than 95%, while some industries or projects require no less than 98%. Breakpoint retransmission should cover at least 72 hours to ensure that missing data can be backfilled after communication is restored. Time synchronization should also be included in commissioning; clock deviation among servers, gateways, and analyzers should preferably not exceed 10 seconds to avoid misalignment of hourly averages.
IV. Routine Maintenance: Use Periodic Operations to Maintain Data Quality
The core of routine maintenance is to keep the sampling path clean, temperature stable, flow normal, and communication online. Operations and maintenance personnel should check carbon dioxide, methane, nitrous oxide, and other greenhouse gas concentrations daily, as well as auxiliary parameters such as oxygen, flue gas flow, temperature, pressure, humidity, and dust. If a device shows abnormal data points for multiple consecutive periods—for example, 15-minute data missing rate exceeds 5%, sampling flow deviates from the setpoint by more than 10%, or heated temperature is below 120 degrees Celsius or above 160 degrees Celsius—an inspection process should be triggered.
Weekly Maintenance
- Check probe purge, filter inspection, pump operating status.
- Monitor standard gas remaining level and expiration dates.
- Replace filter elements if necessary; check pump diaphragms.
- Ensure CO2 standard gas has at least two cylinders available.
Monthly & Quarterly Checks
- System-level check: zero/span drift, tightness, drain valves.
- Cabinet air conditioner status and UPS battery health.
- Annual full-system calibration or metrological verification.
- Compare with manual monitoring data (min. 6 sample sets).
Data quality review is the bridge between routine maintenance and carbon accounting. Operations and maintenance personnel should not only ensure equipment availability but also check whether data logic is reasonable. For example, carbon dioxide concentration and oxygen concentration should show a reasonable correlation, flue gas flow and load should have a consistent trend, and data during boiler start-up/shutdown phases should show clear changes. If data remains constant for a long period, abnormal spikes, negative values, out-of-range values, or mismatched process parameters are found, abnormal data should be promptly flagged, and manual monitoring or process records should be supplemented. For carbon footprint accounting, if abnormal data are directly included in the product life cycle inventory without review, emission intensity may be overestimated or underestimated.
V. Common Fault Troubleshooting: Layered Localization by Symptom
Troubleshooting should proceed systematically based on observed symptoms. Below are six common fault types and their diagnostic paths:
- Complete Data Interruption: Check power supply, circuit breakers, UPS, and sampling pump. Verify gateway indicator lights, switch ports, and signal strength. Confirm PLC/data acquisition module status. Finally, validate platform interface address, port, protocol, and authentication. If local data exists but platform does not, the issue is in communication; if no local data, check sampling/analyzer/power layers.
- Concentration Displayed as Zero or Negative: Zero values may result from probe blockage, water accumulation, filter blockage, or insufficient pump flow. Negative values often stem from zero drift, incorrect standard gas connection, or cross-interference. Inject standard gas via bypass to isolate the problem: if readings normalize, the issue is in the sampling path; if not, check the analyzer/valve/span parameters.
- Elevated Concentration Readings: Causes include standard gas contamination, elevated zero point, heated-line failure causing condensation/adsorption, incorrect moisture compensation, dust scattering, ambient air ingress, or analyzer cross-interference. For IR-based equipment, verify interference compensation for water vapor, SO2, NOx, and CH4. Check heated-line and dehumidification systems if process data shows low temp/high humidity.
- Low Concentration or Lower-than-Expected Readings: Likely due to system leakage, filter blockage, pump diaphragm aging, excessive negative pressure, incorrect dry/wet basis conversion, low span coefficient, or insufficient standard gas concentration. Measure sampling flow, pipeline negative pressure, and oxygen concentration. A simultaneous rise in oxygen suggests air ingress/leakage.
- Severe Data Fluctuation or Frequent Alarms: May reflect actual operational changes or issues like unrepresentative sampling points, eddies, power interference, packet loss, or improper filtering. Evaluate against flow, oxygen, temp, pressure, and load curves. If only one parameter fluctuates, check its sensor wiring/span; if multiple fluctuate, check power, grounding, pump, and network.
- Communication or Data Format Abnormalities: Symptoms include missing minute data, incorrect hourly averages, unit mismatches, timestamp misalignment, or failed breakpoint retransmission. Verify gateway sampling/upload cycles, units, decimals, and time zone settings. Create a data field mapping table during commissioning and set threshold alarms/logic validation on the platform.
VI. Case Study: Linkage of Online Monitoring and Carbon Accounting in a Chemical Industrial Park
A chemical industrial park includes a captive power plant, ammonia synthesis units, and steam boilers, with annual carbon dioxide emissions on the order of hundreds of thousands of tons. The park initially used energy statistics and the emission factor method to account for Scope 1 emissions, but when calculating product carbon footprints, it was difficult to distinguish contributions from different processes and different discharge outlets. To improve data granularity, the park installed eight online greenhouse gas monitoring systems at the main discharge outlets and key process unit outlets. Monitored parameters include carbon dioxide, methane, nitrous oxide, oxygen, flue gas flow, temperature, pressure, humidity, and dust.
During commissioning, the project identified two typical issues. The first was at a boiler discharge outlet, where carbon dioxide readings decreased instead of increasing when load rose. Troubleshooting found liquid accumulation at low points in the heated line; after moisture condensed, it caused partial gas adsorption and increased sampling resistance. After correction, the line slope was adjusted to 2%, the heated temperature stabilized at 140 degrees Celsius, and the data trend returned to normal. The second was at an ammonia synthesis unit discharge outlet, where methane concentration occasionally showed abnormal spikes. Further inspection found insufficient probe purge pressure and dust accumulation on the filter surface, causing short-term uneven sampling. After correction, purge pressure was increased from 0.25 MPa to 0.4 MPa, and abnormal spikes were significantly reduced.
After six months of stable system operation, the park's data completeness rate reached 98.6%, and the average deviation from manual comparison was 4.2%, meeting the project requirement of within 5%. Based on online monitoring data, the park discovered one bypass leak point that had not been fully included in the original energy statistics scope. After correction, the annual carbon dioxide equivalent accounting increased by approximately 11,000 tons. This case demonstrates that online monitoring can not only improve carbon accounting accuracy but also identify process leaks and abnormal emissions, providing data support for equipment maintenance, energy management, and product carbon footprints.
In terms of carbon footprint applications, the park links online monitoring data with the production management system, fuel consumption records, and material balance sheets to generate emission data by unit, time period, and product. For export products or scenarios where supply chain customers require disclosure of carbon emission intensity, enterprises can combine Scope 1 direct emission data with Scope 2 electricity emission data, then add raw material and transportation stage data to build a product carbon footprint inventory. If online monitoring data quality is stable, it can also support low-carbon product certification, green supply chain management, and internal carbon pricing.
VII. Outlook: Online Monitoring Supporting Carbon Footprints and Greenhouse Gas Inventories
In the future, carbon emission monitoring will no longer be merely a standalone equipment project but part of corporate digital infrastructure. With the convergence of online greenhouse gas monitoring, energy management systems, manufacturing execution systems, and carbon management platforms, enterprises are expected to achieve end-to-end data integration from fuel entering the furnace and process emissions to flue gas monitoring and product carbon footprints. For key emission units, high-quality online data will become an important support for carbon accounting, compliance settlement, and methodology verification of emission reduction projects. For supply chain enterprises, traceable emission data will become a foundational capability for responding to green trade rules and downstream customer inquiries.
Technically, high-precision gas analyzers, edge computing, anomaly detection algorithms, and digital twins will further enhance data credibility. For example, equipment status can be judged through multi-parameter coupling, historical operating conditions can be used to identify abnormal data, models can fill short-term gaps, or online monitoring can be combined with drones, plant boundary stations, infrared imaging, and material balance methods to form a "point-line-surface" coordinated greenhouse gas monitoring system. From a standards perspective, enterprises should pay attention to changes in national and industry requirements regarding online monitoring, data validity, calibration cycles, data reporting, and carbon footprint accounting, and adjust operations and maintenance strategies in a timely manner.
From a management perspective, the difficulty of carbon emission monitoring lies not only in the equipment itself but also in cross-departmental collaboration. Environmental protection departments focus on emission compliance, production departments focus on stable operation, energy departments focus on load and efficiency, finance departments focus on carbon assets and costs, and supply chain departments focus on product carbon footprints. Only by integrating installation, commissioning, maintenance, fault handling, and carbon accounting into a unified process can common problems be avoided, such as equipment being online but data unusable, data usable but unable to enter accounting, or accounting completed but difficult to trace. The value of carbon emission monitoring ultimately lies in helping enterprises transform "invisible emissions" into data assets that are "manageable, optimizable, and reportable."